


Absolute Precision
In a corner of Christchurch, New Zealand, bronze engineering company AW Fraser turns 100 tonnes of recycled metal scrap a week – shell casings, copper pipe, car radiators, cable off-cuts – into shiny precision-machined OEM components.
In a corner of Christchurch, New Zealand, bronze engineering company AW Fraser turns 100 tonnes of recycled metal scrap a week – shell casings, copper pipe, car radiators, cable off-cuts – into shiny precision-machined OEM components.
New Zealand-based AW Fraser is an all-in-one copper alloy foundry, extrusion mill and modern CNC machine shop. The recycled material is converted on site into 40 different types of highly specified bronze and brass alloys. Some 50 percent of the manufactured bar is exported, while the rest is machined into specialized OEM components for blue-chip companies around the world.
From this far corner of the world, AW Fraser supplies gear blanks to SEW Eurodrive in Germany, machined components to construction companies Caterpillar, Hitachi, Yamaha and Mercury Marine, and components for rail engines and braking systems. In all, 90 percent of AW Fraser production is exported to 35 countries.
“We are diverse in terms of the industries we supply to,” says CFO Paul Isitt, part-owner and a director of the company. “We have to be responsive and remain competitive. Focus on continuous improvement is what drives us every day. Our core principle is that we want to be the best, because we are working with some of the best companies in the world.”
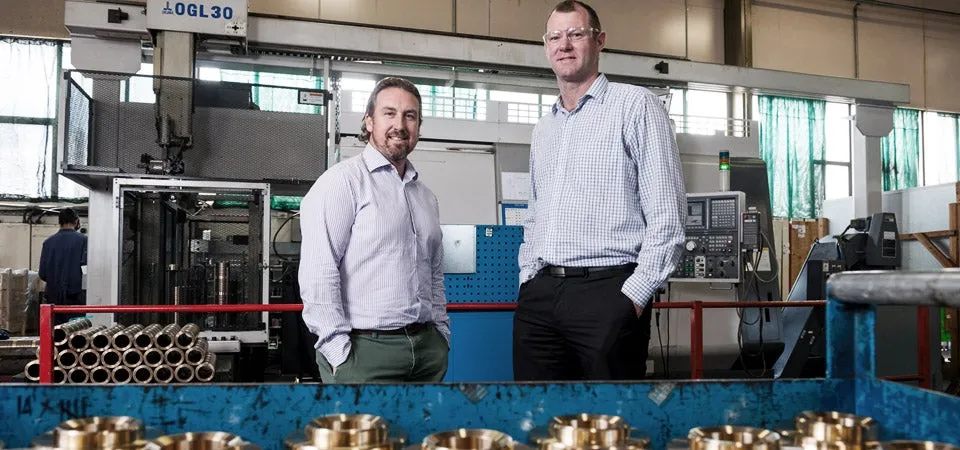
The company is a low- to medium-volume manufacturer. “The parts we manufacture range from small runs, in twos and threes, of highly specialized components to longer runs of 40,000, so for us, standardization and repeatability are critical,” Isitt says.
As part of the Sandvik Coromant Preferred Supplier Program, Sandvik Coromant account manager Clinton LeRoux works closely with Jody Tuckwell. AW Fraser, machine shop manager, and the engineering team to achieve process improvements and standardization.
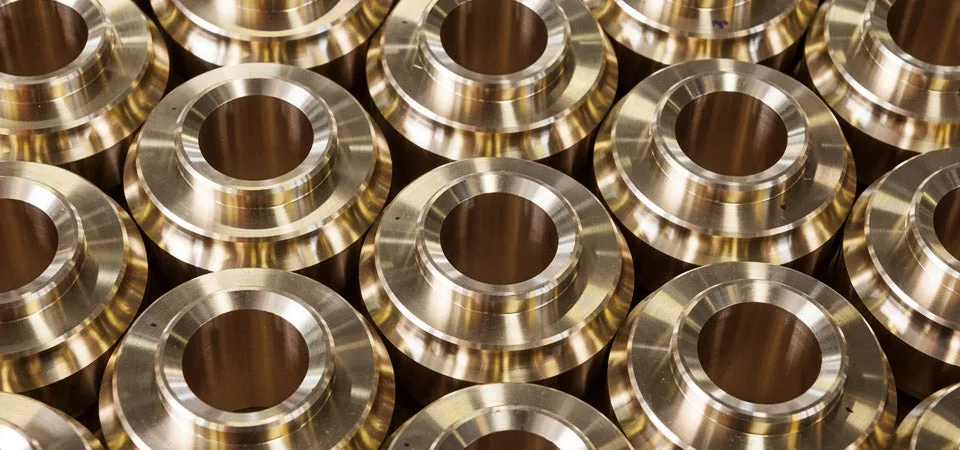
AW Fraser wanted to improve speed, repeatability and standardization of setups in short run-time jobs of highly specialized components. “We are always looking for ways to be better both in terms of efficiency on the floor and in our technology and systems,” says Jody Tuckwell.
“We sometimes make a specialized product in twos or threes, and it might be a year before we do it again,” he explains. “We are working to a 15-micron tolerance in run sizes varying from two to 1,200. We work with absolute precision.
“We’re looking for multiple micro-successes, which can accumulate into larger numbers of hours saved,” he continues. “We try to identify the parts of the process where we have the most to gain from improvement. The parting system was one – the material was brittle and sticky.”
AW Fraser undertook testing with the new CoroCut QD parting system combined with the Coromant Capto tooling system on one of AW Fraser’s CNC lathes on a six-month trial.
“The time to switch a machine went from one to two hours down to 15 minutes,” Tuckwell says. “That’s 750 setup hours per year on one machine.”
Following the success with the retrofitted machine, AW Fraser invested in two new fully integrated Okuma CNC multi-tasking machines, fully fitted with Capto and the CoroCut QD, taking the total machine count to 30.
“But the biggest gain was for our operators,” Tuckwell says. “They feel confident with the new system. We try to make sure that the guys enjoy what they do. It is a change for them. They put tools in, put new jaws in, put work in the machine and push go – that’s huge.”
Technical insight
Standardization of process and repeatability are key in achieving profitability in small runs of highly specialized components. At AW Fraser, parting off time in small runs of two to 15 components was reduced by 50 percent with the new CoroCut QD parting off system optimized for bar fed machines.
Machine shop manager Jody Tuckwell says they have also condensed the 10 or 12 different inserts down to four widths, which has reduced inventory. “Monthly use of inserts has decreased, and there may also be some increase in feed rate, tool life and security of process,” he says.
CoroCut QD combines high-precision coolant with parting off inserts, chip-breaking geometries and wiper inserts for improved surface quality at high feeds. Stable, user-friendly clamping means no torque wrench is needed, and the rail insert seat ensures stable, precise insert position.
CoroCut QD was combined with the Coromant Capto modular quick-change tooling system, allowing the same tools to be used on all three machines. The Coromant Capto is an integrated and modular tool face that holds to the ISO 26623 standard for tool-holding systems. Its quick-change tool holders reduce setup and tool change time, allowing standardization of tools across machines.
AW Fraser
New Zealand-based AW Fraser was founded in 1939 and has 180 employees. The combined foundry, extrusion mill and CNC shop works 24/7 on various shift patterns. In 2006 it became fully management owned.
