 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


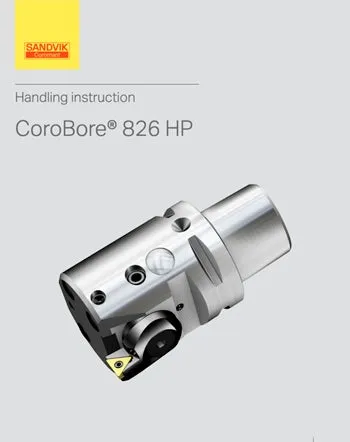
CoroBore® 826
Fine boring tool with excellent chip control
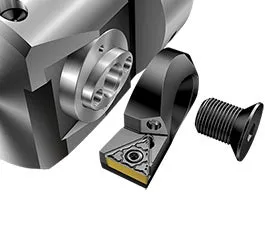
Mounting of cartridge
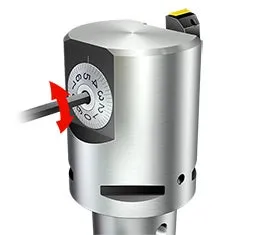
Tool setting of diameter
Diameter and counterweight setting
For diameter 92-154 (3.662-6.063 inch)
|
1
|
3
|
|
2a
|
4
|
|
2b
|
5
|
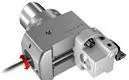
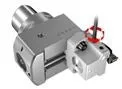
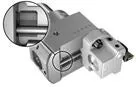
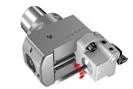
- Unlock counter weight locking screw.
- Set the internal counterweight by adjusting screw (2a) until requested cutting diameter (nominal value) is aligned with the mark (2b) on top of the tool.
- Lock the counterweight with appropriate torque, 6 Nm (4.425 ft/lbs).
Mount the cartridge on the fine boring head with correct torque, 6 Nm (4.425 ft/lbs).
Assemble the fine boring head on adaptor.
Adjust the diameter by moving the fine boring head with the side screw until requested cutting diameter (nominal value) is aligned with the scale visible on adaptor. - Tighten the fine boring head screws with correct torque, 14 Nm (10.236 ft/lbs).
- Fine adjust the diameter with the 826 scale.
Lock fine boring head with correct torque, 8 Nm (5.900 ft/lbs).
See
Achieving close hole tolerances for more information.
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant Finland
+358942451675AB Sandvik Coromant, 811 81 Sandviken, Sweden