 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


CoroBore® BR20
Twin-edge rough boring tools for flexible boring


Torque
Always use a torque wrench and apply recommended torque on screws for insert and tool assembly torque.

Clamping
Do not clamp damped Silent Tools™ straight over the adaptor body.

Laser-marked scale
The laser-marked scale on the adaptor facilitates setting the diameter.


Application tips
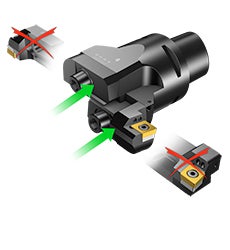
Tool setting for back boring
• Remove grub screw from top cutting fluid outlet and attach it into lower cutting
• Fluid outlet in order to get correct coolant position
• Rotate cartridge 180°
• Use slide extension if needed
• Reverse rotation direction
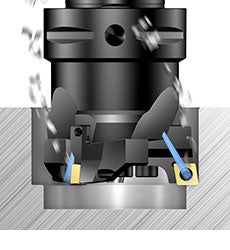
Blind hole
When machining a blind hole it is very important to secure that proper chip evacuation takes place.
Correct cutting data is essential to achieve proper chip forming
Ensure/check that the chips do not jam or wear the inserts
Coolant pressure and flow should be sufficient to evacuate the chips
Vertical machines are more critical than horizontal machines for efficient chip evacuation
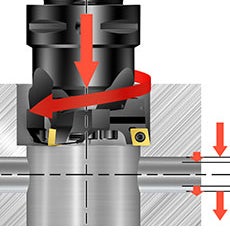
Interrupted cuts
Machining of interrupted cuts, such as cross holes, set high demands on insert cutting conditions.
Choose a tough grade
Choose a strong, square negative basic-shaped insert for improved process security, valid for stable conditions
Reduce cutting data if there are severe interruptions
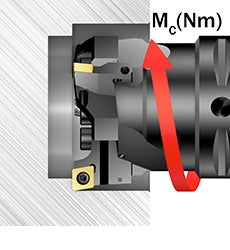
Weak machines
When roughing, make sure the machine has the required power and torque needed for the specific boring application. Feed, number of inserts, hole diameter and depth of cut are main affecting parameters.
Recommendations
General recommendations rough boring:
- Starting data: vc 200 m/min (valid when vc on insert box is bigger than vc 200 m/min) at short overhang. Check insert box for feed and depth of cut recommendations
- vc = 50% of recommended data on label. If vibrations occur, reduce speed and increase feed. Do not use max recommended feed and ap at the same time
- Usable length to diameter ratio (ULDR) = Boring depth LU / Boring diameter DC
Cutting data: CoroBore® 111
| Order code | Grade | Feed range (fn) | Depth of cut (ap) | Cutting speed (vc) | ||||||
| Min | Max | Recommended | Min | Max | Recommended | Min | Max | Recommended | ||
| SPMT0606-BR | 4425 | 0.10 | 0.25 | 0.20 | 0.6 | 4.5 | 2.0 | 365 | 460 | 395 |
| SPMT0606-BM | 2025 | 0.10 | 0.15 | 0.10 | 0.6 | 4.5 | 1.8 | 260 | 265 | 265 |
| SPMT0606-BR | 3210 | 0.15 | 0.30 | 0.25 | 0.6 | 4.5 | 2.0 | 285 | 330 | 300 |
| SPMT0606-BM | 1145 | 0.10 | 0.15 | 0.10 | 0.6 | 4.5 | 1.8 | 15 | 20 | 20 |
| SPMT0808-BR | 4425 | 0.15 | 0.35 | 0.20 | 0.8 | 6.5 | 2.5 | 325 | 425 | 395 |
| SPMT0808-BM | 2025 | 0.10 | 0.25 | 0.20 | 0.8 | 6.5 | 2.2 | 225 | 265 | 240 |
| SPMT0808-BR | 3210 | 0.20 | 0.50 | 0.30 | 0.8 | 6.5 | 2.5 | 235 | 315 | 285 |
| SPMT0808-BM | 1145 | 0.10 | 0.15 | 0.10 | 0.8 | 6.5 | 2.2 | 15 | 20 | 20 |
| SPMT1212-BR | 4425 | 0.15 | 0.40 | 0.25 | 1.2 | 9.0 | 3.0 | 305 | 425 | 365 |
| SPMT1210-BM | 2025 | 0.10 | 0.30 | 0.20 | 1.0 | 9.0 | 2.5 | 205 | 265 | 240 |
| SPMT1212-BR | 3210 | 0.20 | 0.50 | 0.30 | 1.2 | 9.0 | 3.0 | 235 | 315 | 285 |
| SPMT1210-BM | 1145 | 0.10 | 0.20 | 0.15 | 1.0 | 9.0 | 2.5 | 10 | 20 | 15 |
| SPMT1812-BR | 4425 | 0.20 | 0.40 | 0.30 | 1.2 | 12.0 | 3.8 | 305 | 395 | 345 |
| SPMT1810-BM | 2025 | 0.20 | 0.30 | 0.25 | 1.0 | 12.0 | 3.0 | 205 | 240 | 225 |
| SPMT1812-BR | 3210 | 0.25 | 0.50 | 0.30 | 1.2 | 12.0 | 3.8 | 235 | 300 | 285 |
| SPMT1810-BM | 1145 | 0.10 | 0.20 | 0.15 | 1.0 | 12.0 | 3.0 | 10 | 20 | 15 |
Tightening torque
Insert screw
| ISO | ANSI | Non ISO | Code | Size | Torx Plus | Nm | Ft/lbs |
| CC06 | CC2(1.5) | 5513 020-03 | M2,5 | 7IP | 0.9 | 0.7 | |
| CC09 | CC09 | 5513 020-09 | M3,5 | 15IP | 3.0 | 2.2 | |
| CC12 | CC43 | 5513 020-17 | M4x0,5 | 15IP | 3.0 | 2.2 | |
| SP06 | 5513 020-33 | M2,2 | 7IP | 0.8 | 0.59 | ||
| SP08 | 5513 020-57 | M3 | 9IP | 1.7 | 1.25 | ||
| SP12 | 416.1-833 | M3,5 | 10IP | 2 | 1.48 | ||
| SP18 | 5513 020-25 | M4 | 15IP | 3 | 2.2 | ||
| SN15 | SN54 | 5512 086-03 | M6 | 20IP | 6.4 | 4.7 | |
Maximum cutting torque and RPM
| Kit product codes | Adaptors | Max cutting torque | Max RPM | |
| Nm | ft-lb | |||
| BR20D-29CC06F/SP06Y-C4L | C4-BR20D-A-189 | 100 | 74 | 15000 |
| BR20D-36CC06F/SP06Y-C3L | C3-BR20D-B-205 | 165 | 122 | 11000 |
| BR20D-45CC09F/SP08Y-C3L | C3-BR20D-C-208 | 290 | 214 | 9000 |
| BR20D-45CC09F/SP08Y-C4L | C4-BR20D-C-257 | 290 | 214 | 9000 |
| BR20D-45CC09F/SP08Y-C6L | C6-BR20D-C-284 | 290 | 214 | 11000 |
| BR20D-56CC09F/SP08Y-C4L | C4-BR20D-D-207 | 350 | 258 | 12000 |
| BR20D-56CC09F/SP08Y-C5L | C5-BR20D-D-323 | 350 | 258 | 7000 |
| BR20D-56CC09F/SP08Y-C6L | C6-BR20D-D-350 | 350 | 258 | 8000 |
| BR20D-71CC12F/SP12Y-C5M | C5-BR20D-E-282 | 580 | 428 | 7000 |
| BR20D-71CC12F/SP12Y-C6M | C6-BR20D-E-382 | 580 | 428 | 7000 |
| BR20D-90CC12F/SP12Y-C6M | C6-BR20D-F-380 | 780 | 575 | 5000 |
| BR20D-90CC12F/SP12Y-C8M | C8-BR20D-F-480 | 780 | 575 | 4000 |
| BR20D-116CC12F/SP12Y-C8S | C8-BR20D-G-388 | 940 | 693 | 5000 |
| BR20D-116CC12F/SP12Y-C8M | C8-BR20D-G-478 | 940 | 693 | 4000 |
| BR20D-150CC12F/SP12Y-C8M | C8-BR20D-H-478 | 1000 | 738 | 4000 |
CoroBore® BR20/CoroBore® BR20 with Silent Tools™ technology
| Insert 90° | Insert 84° | ||||||||||
| Size | DCN (mm) | DCX (mm) | ISO | ANSI | Nm | Ft/lbs | Screw size | Non-ISO | Nm | Ft/lbs | Screw size |
| A | 23 | 29 | CC06 | CC2(1.5) | 4.8 | 3.5 | M4 | SP06 | 4.8 | 3.5 | M4 |
| B | 28 | 36 | CC06 | CC2(1.5) | 4.8 | 3.5 | M4 | SP06 | 4.8 | 3.5 | M4 |
| C | 35 | 45 | CC09 | CC3(2.5) | 9 | 6,6 | M5 | SP08 | 9 | 6,6 | M5 |
| D | 44 | 56 | CC09 | CC3(2.5) | 16.0 | 11.8 | M6 | SP08 | 16.0 | 11.8 | M6 |
| E | 55 | 71 | CC12 | CC43 | 38.0 | 28.0 | M8 | SP12 | 38.0 | 28.0 | M8 |
| F | 70 | 90 | CC12 | CC43 | 75 | 55 | M10 | SP12 | 75 | 55 | M10 |
| G | 89 | 116 | CC12 | CC43 | 75 | 55 | M10 | SP12 | 75 | 55 | M10 |
| H | 115 | 150 | CC12 | CC43 | 75 | 55 | M10 | SP12 | 75 | 55 | M10 |
Tool holding
Bending stiffness and torque transmissions are the most important factors when choosing a tool holder for boring operations. First choice should always be tools with
Coromant Capto® coupling, which offers excellent repeatability and the best stability characteristics on the market. Use only one adaptive item between the Silent Tools™ adaptor and the machine tool spindle.
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant UK
+44 (0)121 368 0305AB Sandvik Coromant, 811 81 Sandviken, Sweden