 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


CoroBore® BR20
Twin-edge rough boring tools for flexible boring
Application test: Differential pitch
®CoroBore BR20 and DuoBore™ * comparison
| Material: | 42CrMo4 soft, P2.1.Z.AN |
| Machine: | Vertical milling machine |
| Machine interface: | ISO 50 |
| Coolant: | No |
| Diameter range: | 55–70 mm (2.17–2.76 inch) |
| Insert: | CCMT 12 04 08-PM 4325 |
| Kappa (Kr): | 90° |
+30%
INCREASED OVERHANG
| DuoBore™ | CoroBore® BR20 | |
| Basic holder | C5-390.00-50 030 | C5-390.00-50 030 |
| Extension | C5-391.01-50 080A | C5-391.01-50 080A |
| Boring tool assembly | 821-70CC12-C5 | BR20-71CC12F-C5 |
| LF (mm) | LU (mm) | vc (m/min) | fz (mm/z) | ap (mm) | n (min-1) | vf (mm/min) | Surface finish | |
| DuoBore™ | 260 | 244.8 | 166.8 | 0.18 | 2.3 | 900 | 500 | Heavy vibration marks |
| CoroBore® BR20 | 316 | 300.8 | 166.8 | 0.18 | 2.3 | 900 | 500 | Shining |
Results
Thanks to the differential pitch, CoroBore® BR20 could increase the overhang with 30% compared to DuoBore™. Comparing the same cutting data, DuoBore™ stopped to perform at LF = 260 mm (10.2 inch), while CoroBore® BR20 reached an LF = 316 mm (12.4 inch) with a shiny surface finish.
*DuoBore is part of the previous generation of rough boring tools from Sandvik Coromant.
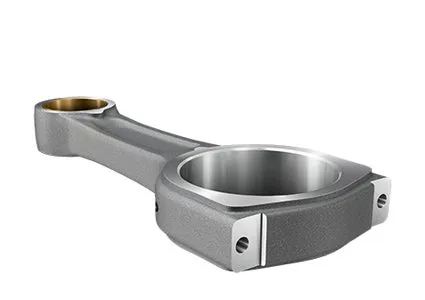
Case: CoroBore® BR20
Challenge: Machining a connecting rod in weak machining conditions. The customer required a stable and secure machining process, good chip control and long insert life and tool life, while obtaining a high surface quality.
| Component: | Connecting rod |
| Material: | C70S6; CMC: 02.2, MC: P2.5.Z.HT, hardness HB280~310 |
| Operation: | Semi-finishing after an initial rough boring operation performed with a combination tool with chamfer |
| Machine: | Feeler VMP-40A, BT40 |
| Coolant | Internal coolant, 15 bar |
| Output power | 11 kW |
| DC, mm (inch) | 59.6 (2.35) |
+75%
INCREASED TOOL LIFE
| Competitor tool | ®CoroBore BR20 | |
| Total length: | 120 mm | 120 mm |
| Machine interface adaptor | C5-390B.555-40 050 | |
| Boring tool assembly | BR20-71SP12Y-C5 | |
| Insert | SPMT 12 12 – BR 4325 (CoroBore® 111) | |
| Kappa (Kr) | 75° | 84° |
| Cutting data | |
| zn | 2 |
| n, rpm | 1500 rep/min |
| vc, m/min (ft/min) | 280 (919) |
| fz mm/rpm (in/rev) | 0.09 (0.0035) |
| ap mm (inch) | 1.2 mm (0.047) |
| Depth of hole, mm (inch) | 31 (1.22) |
Results
CoroBore® BR20 together with CoroBore® 111 inserts achieved good surface finish, excellent chip breaking and 70% increased tool life compared to existing tooling solution. The customer can now produce 700 pieces instead of 400 pieces within the same time.
Customer case: CoroBore® BR20 with CoroBore® 111 inserts
| Customer demands: | Large cutting depths |
| Component: | Connecting rod |
| Material: | C70S6BY; CMC: 02.2, MC: P2.5.Z.HT |
| Hardness: | HB280~310 |
| Operation: | Rough boring |
| Machine: | HYUNDAI WIA F650, BT50 |
| Coolant: | Internal coolant 30 bar |
| Output power: | 22 KW |
| Machining conditions: | Interrupted cut, uneven allowance |
| DC: | 56 mm (2.20) |
+20%
TOOL LIFE
| Reference tool 140 mm | ®CoroBore BR20 190 mm | |
| Basic holder | C5-390B.58-50 040 | |
| Extension | C5-391.01-50 080A | |
| Boring tool | Solid boring tool with BT50 spindle coupling | Tool assembly code: BR20-71SP12Y-C5 Adaptor: C5-BR20-E-048 Slide: BR20-EA-SP12Y-18 & BR20-EB-SP12Y-18 |
| Insert | CoroBore 111 | |
| Kappa (Kr) | 75° | 84° |
| Cutting data | |
| zn | 2 |
| n, rpm | 1100 rep/min |
| vc, m/min (ft/min) | 190 (623) |
| fn mm/rev (in/rev) | 0.11 (0.004) |
| ap mm (inch) | 5 (0.197) |
Results:
- Customer is very satisfied with CoroBore® BR20 and the CoroBore® 111 insert, as it can take large cutting depths, gives a good surface finish, ensures good chip control and tool life can be increased by +20%.
- Customer can now produce 350 pieces instead of 280 pieces within the same time. Notch wear pattern (after 350 pieces) was achieved with the CoroBore®
- The customer could produce in total 1400 components with the CoroBore® BR20 tool.
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

AB Sandvik Coromant, 811 81 Sandviken, Sweden