 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


CoroMill® 490
First choice for general and repeated shoulder milling

Select the right insert geometry
Light (-L) Medium (-M) Heavy (-H)

How to choose the right pitch
When choosing the most suitable number of effective cutting edges, zc, for the operation, it is essential to consider the pitch (distance between the cutting edges).

Select the right tool holding
Tool mounting has the greatest influence on the milling result. The larger the cutting depth, the more important the size and stability of the coupling become, since the radial forces are considerable when using shoulder face mills, particularly long edge milling cutters.

Cutting depth
Insert size 08 Insert size 14

Application tips
Application checklist and hints
What to consider when performing a shoulder milling operation? Find some useful tips and tricks here.
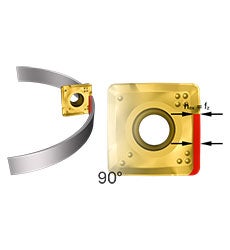
Chip formation
Successful chip formation and chip evacuation is the key to high-quality milling operations. Learn more about how to form the perfect chips, and don’t forget the golden rule: Thick to thin.
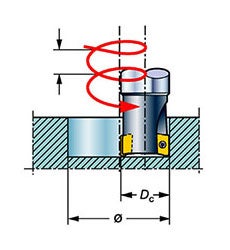
Cutter position
Each time a milling edge enters a cut, it is subjected to a shock load. The right type of contact between edge and material at the entry and also at the exit of a cut must be considered for successful milling.
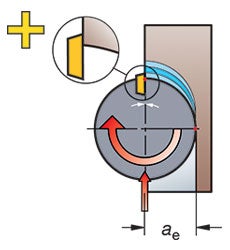
Entering the component
Shoulder milling often uses a low radial engagement, therefore it is important to consider feed per tooth (fz) vs. maximum chip thickness (hex).
Calculating cutting parameter according to right hex value will ensure good cutting action with better surface quality and tool life.
Recommendations
Cutter body selection
●
Difficult conditions

L
Limited stability and power
Deep full-slotting operations
Lowest cutting forces
◐
Average conditions

M
General purpose
○
Good conditions

H
Short chipping materials
Heat resistant materials
Edging operations
First choice insert
| Roughing | M-PH 4340 | M-MM 1040 | M-PH 3330 | E-ML H13A | M-MM S40T | M-PM 1010 |
| Medium | M-PM 4330 | E-MM 1040 | M-KM 3330 | E-ML H13A | E-MM S30T | M-PM 1010 |
| Finishing | M-PL 1130 | E-ML 1040 | M-KL 1020 | E-ML H13A | E-ML S30T | M-PL 1010 |
| P | M | K | N | S | H |
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant UK
+44 (0)121 368 0305AB Sandvik Coromant, 811 81 Sandviken, Sweden