 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


How to use

The hole
For basic hole size calculations, use the appropriate formulas for cutting taps. D = Hole diameter (mm, inch
TD = Nominal thread diameter (mm, inch
TP = Thread pitch (mm, inch)

The component
When the hole is analyzed, have a look at the workpiece material, component shape, and quantity

The machine
The machine influences: Always consider:

Tool holding
The CoroChuck™ 970 is designed for stable and precise tapping in all materials. It improves tap tool life, surface quality, and offers the highest process security.
Coolant
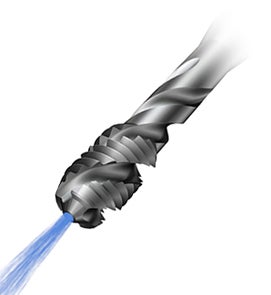
Coolant is critical to a successful tapping operation. The coolant supply influences chip evacuation, thread quality and tool life.
Keys to a successful tapping operation
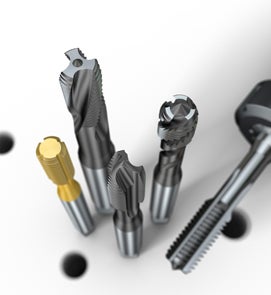
To ensure a good tapping operation and a high-quality finished product, follow these steps.
Threading chamfer type
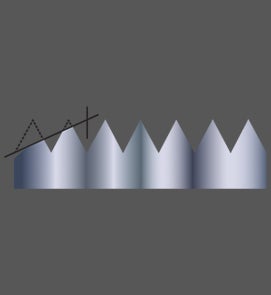
The type of hole to be tapped determines which chamfer type is best suited for use. There are two different chamfer types C and E.
Which tap and cutting speed should you choose?
General speeds can be found in the catalogue, consider the recommended as a safe start value
Useful apps
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant UK
+44 (0)121 368 0305AB Sandvik Coromant, 811 81 Sandviken, Sweden