 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


CoroTurn® Prime
All-directional turning

Entry to workpiece
Always use feed reduction and radius entry when going into the material. Use CoroPlus® Tool Path for PrimeTurning™ for correct programming codes and techniques.

Chip thickness (hex)
Keep chip thickness constant by reducing feed for downward moves. Use CoroPlus® Tool Path for PrimeTurning™ for correct programming codes and techniques.

Coolant benefits
Under coolant is advantageous to achieve longer tool-life while over coolant is beneficial for forming thinner chips.
Application tips
Cutting data application area for A-type and B-type
| Depth of cut (ap) | |
 |
Feed (fn) |
Note: Using inserts at higher ap and fn leads to risk for overload and at lower ap and fn there is a risk for long chips.

Cutting data application area for A-type geometries

P*) Low-carbon and high-strength/ductile steel
P**) Alloy steel
M*) Austenitic stainless steel
M**) Duplex stainless steel
K*) Nodular cast iron
K**) Grey cast iron
S*) HRSA
S**) Titanium
Cutting data application area for B-type geometries

P*) Low-carbon and high-strength/ductile steel
P**) Alloy steel
M*) Austenitic stainless steel
M**) Duplex stainless steel
K*) Nodular cast iron
K**) Grey cast iron
S*) HRSA
S**) Titanium
Recommendations
CoroTurn Prime A-type
Insert grade
| Machining conditions | P | M | K | S, HRSA |
S, Ti |
| Good | 4415 | 2025 | 4415 | 1210 | H13A |
| Average | 4425 | 2025 | 4425 | 1115 | H13A |
| Difficult | 2025 | 2025 | 2025 | 2025 | 1115 |
Insert geometry
| Operation | P* | P** |
M* | M** |
K* | K** |
S* | S** |
| Finishing | L3 | L5W | L5W | L3 | L5W | L5W | L5W | L3 |
| Medium | L3 | L5 | L5 | L5 | L5 | L5 | L5 | L5 |
P*) Low-carbon and high-strength/ductile steel
P**) Alloy steel
M*) Austenitic stainless steel
M**) Duplex stainless steel
K*) Nodular cast iron
K**) Grey cast iron
S*) HRSA
S**) Titanium
CoroTurn Prime B-type
Insert grade
| Machining conditions | P | M | K | S, HRSA |
S, Ti |
| Good | 4415 | 2220 | 4415 | 1210 | H13A |
| Average | 4425 | 2220 | 4425 | 1115 | H13A |
| Difficult | 2025 | 2025 | 2025 | 2220 | 1115 |
Insert geometry
| Operation | P* | P** |
M* | M** |
K* | K** |
S* | S** |
| Finishing | L4W | M5W | M5W | L4W | M5W | M5W | M7W | L4W |
| Medium | L4 | M5 | M5 | M7 | M5 | M5 | M5 | L4 |
| Roughing | M7 | M5 | M5 | M7 | M5 | M5 | M7 | M7 |
P*) Low-carbon and high-strength/ductile steel
P**) Alloy steel
M*) Austenitic stainless steel
M**) Duplex stainless steel
K*) Nodular cast iron
K**) Grey cast iron
S*) HRSA
S**) Titanium
First choice |
Second choice |
||
External turning |
Internal turning |
||
 Side backward (SBW) |
 Side forward (SFW) |
 End backward (EBW) |
 Side forward (SFW) |
 End backward (EBW) |
 End forward (EFW) |
 Side backward (SBW) |
 End forward (EFW) |
Cutting data recommendations
External turning
A-type CP-A11xx-xxx
 |
SBW | EBW | SFW | EFW | |
| fn min | 0.2 (.0079) | 0.2 (.0079) | 0.1 (.0039) | 0.1 (.0039) | |
| fn rec | 0.4 (.0157) | 0.4 (.0157) | 0.2 (.0079) | 0.2 (.0079) | |
| fn max | 0.5 (.0197) | 0.5 (.0197) | 0.25 (.0098) | 0.25 (.0098) | |
| ap min | 0.25 (.010) | 0.25 (.010) | 0.25 (.010) | 0.25 (.010) | |
| ap rec | 1.5 (.059) | 1.5 (.059) | 1 (.039) | 1 (.039) | |
| ap max | 3 (.118) | 2.5 (.098) | 1.5 (.059) | 1.5 (.059) | |
| KAPR | 30 | 25 | 115 | 120 | |
| RMPX | 15 | 10 | 15 | 10 |
B-type CP-B11xx-xxx
 |
SBW | EBW | SFW | EFW | |
| fn min | 0.3 (.0118) | 0.3 (.0118) | 0.2 (.0079) | 0.2 (.0079) | |
| fn rec | 0.6 (.0236) | 0.6 (.0236) | 0.35 (.0138) | 0.3 (.0118) | |
| fn max | 1.2 (.0472) | 1.2 (.0472) | 0.6 (.0236) | 0.6 (.0236) | |
| ap min | 0.5 (.020) | 0.5 (.020) | 0.5 (.020) | 0.5 (.020) | |
| ap rec | 2 (.079) | 2 (.079) | 2 (.079) | 2 (.079) | |
| ap max | 4 (.157) | 4 (.157) | 3 (.118) | 3 (.118) | |
| KAPR | 25 | 25 | 95 | 95 | |
| RMPX | 23 | 23 | 23 | 23 |
Internal turning
A-type CP-A11xx-xxx
 |
SBW | EBW | SFW | EFW | |
| fn min | 0.2 (.0079) | 0.2 (.0079) | 0.1 (.0039) | 0.1 (.0039) | |
| fn rec | 0.4 (.0157) | 0.4 (.0157) | 0.2 (.0079) | 0.2 (.0079) | |
| fn max | 0.5 (.0197) | 0.5 (.0197) | 0.25 (.0098) | 0.25 (.0098) | |
| ap min | 0.25 (.010) | 0.25 (.010) | 0.25 (.010) | 0.25 (.010) | |
| ap rec | 1.5 (.059) | 1.5 (.059) | 1 (.039) | 1 (.039) | |
| ap max | 2.5 (.098) | 3 (.118) | 1.5 (.059) | 1.5 (.059) | |
| KAPR | 25 | 30 | 120 | 115 | |
| RMPX | 10 | 15 | 10 | 15 |
B-type CP-B11xx-xxx
 |
SBW/EBW | SFW | EFW | |
| fn min | 0.3 (.0118) | 0.2 (.0079) | 0.2 (.0079) | |
| fn rec | 0.6 (.0236) | 0.3 (.0118) | 0.35 (.0138) | |
| fn max | 1.2 (.0472) | 0.6 (.0236) | 0.6 (.0236) | |
| ap min | 0.5 (.020) | 0.5 (.020) | 0.5 (.020) | |
| ap rec | 2 (.079) | 2 (.079) | 2 (.079) | |
| ap max | 4 (.157) | 3 (.118) | 3 (.118) | |
| KAPR | 25 | 95 | 95 | |
| RMPX | 23 | 23 | 23 |
Where to apply PrimeTurning™
External turning
Best suited for short and compact components and slender ones using tail stock
Suitable |
Not suitable |
| Short and compact components | Components without tail-stock |
 |
 |
| Components with tail-stock | |
 |
|
Minimum diameter
Clearance on the insert and holders makes it difficult to start at less D min3 diameter in EBW (End backward) direction. However there are no limits when facing in EFW (End forward) direction i.e. conventional way.

| D min3 | ||
| EBW | EFW | |
| A-type | 30 (1.18") | 0 |
| B-type | 30 (1.18") | 0 |
Internal turning
CoroTurn® Prime SL heads can be used for internal turning of diameters above 40 mm (1.575 inch) and overhangs up to 8–10×D

Ensure optimal performance and avoid issues by considering Dmin when using Silent Tools boring bars. Tangential and radial deflection, influenced by bar design, overhang, and cutting force, can lead to clearance loss.
Highlights
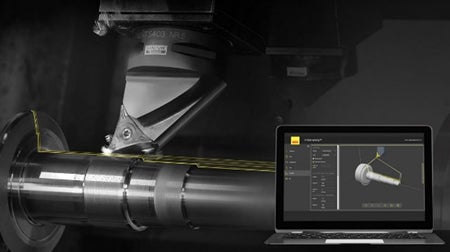
Optimize your tool path
The CoroPlus® Tool Path software is updated with many new features to secure maximum output for your PrimeTurning™ applications. Try out the one-month free trial of the CoroPlus® Tool Path software and see it for yourself!
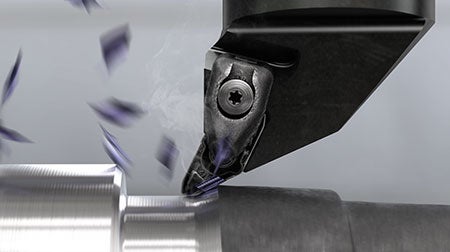
The geometry for finishing operations in ductile materials
The -L4 geometry is optimized for machining low-carbon and high-strength steel, duplex stainless steel and titanium at low to medium feed rates. The geometry delivers outstanding productivity even at lower feed rates, due to increased cutting speed and/or longer tool life compared to conventional turning.
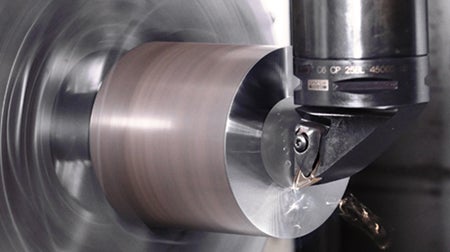
The geometry for difficult-to-machine materials
Achieving good chip control has always been difficult in low-carbon and high-strength steels. The -H3 geometry is optimized for these materials, eliminating concerns about chip control.
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant UK
+44 (0)121 368 0305AB Sandvik Coromant, 811 81 Sandviken, Sweden