 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


T-Max® P
T-Max® P is your first choice for external general turning, designed for metal cutting in a wide range of applications. It delivers stability and productivity, making it ideal for turning of medium and large components even if demanding roughing operations and materials.

Insert seat
Clean and inspect insert seat for damaged locations and support for cutting edge

Shims and shim seats
Ensure that shim corners have not been knocked off during machining or handling and shim seats should have no edge build up

Contact faces
Check supporting and contact faces, making sure there is no damage or dirt.

Clamping
In boring operations, it is important to have the best possible clamping. If not supported, overhang will be increased and might create vibration.

Application tips
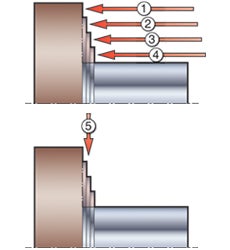
Avoid chip jamming
Turn towards shoulder (steps 1 – 4) and stop before the final dimension of the shoulder. Keep the same feed rate for all four steps to avoid chip jamming. The final cut (5) of the shoulder is recommended to be done in one vertical cut starting from outer diameter towards inner diameter.
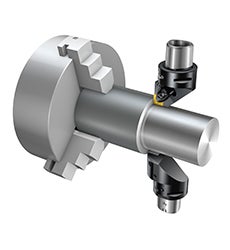
Avoid vibrations
Machines with two turrets, upper and lower turret, is recommended to avoid vibrations. The set up will level out the forces and stabilize the whole process avoiding vibration and bending of the part.
Recommendations
Insert and system
External operation
| Finishing | Medium | Roughing | |
| Insert shape | C | C | C |
| Insert size | 12 | 12 | 12 |
| Entering angle | 95° | 95° | 95° |
| Clamping | Lever | Lever | Lever |
Internal operations
| Fishing | Medium | Roughing | |
| Insert shape | C | C | C |
| Insert size | 12 | 12 | 12 |
| Entering angle | 95° | 95° | 95° |
| Clamping | Lever | Lever | Lever |
Insert grade
| Machining conditions | P | M | K | S | H |
| Good | GC4415 | GC2220 | GC3210 | GC1105 | CB7115 |
| Average | GC4425 | GC2025 | GC3210 | GC1115 | CB7125 |
| Difficult | GC4335 | GC2035 | GC3225 | GC1125 | CB7135 |
Insert geometry
| Operation | P | M | K | S | H |
| Finishing | -PF | -MF | -KF | -SF | S01525 |
| Medium | -PM | -MM | -KM | -SM | S01525 |
| Roughing | -PR | -MR | -KR | -SMR | S02035 |
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Coromant UK
+44 (0)121 368 0305AB Sandvik Coromant, 811 81 Sandviken, Sweden