 close
- Productschevron_right
- Learningchevron_right
- Manufacturing solutionschevron_right
- Supportchevron_right


CoroTurn® TR
Stable external and internal profiling
Customer case
Finishing with CoroTurn® Hard PrimeTurning
Tool life increase
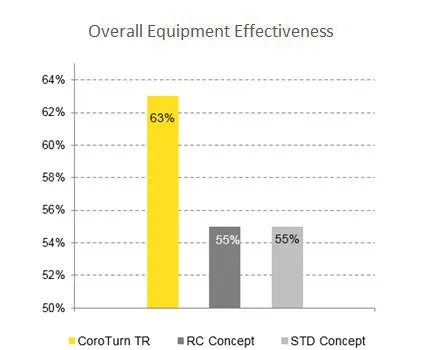
Productivity
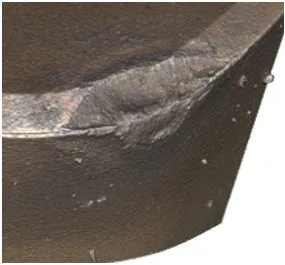
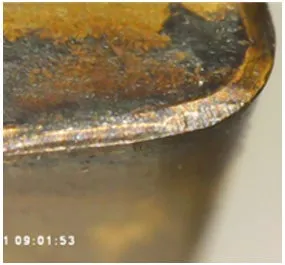
| Component | Input shaft | |
| Material | H1.3.Z.HA, 16MnCr5, 60HRC (case hardened) | |
| Operations | Finishing (Rz max. 4) | |
| Machine | EMAG VTC |
Challenge: Customer looked for a solution to increase productivity and to reach higher component output.
Result: By changing to CoroTurn® TR, the customer experienced a significant increase in tool life and reduced cycle time, resulting in increased productivity.
| Competitor | Sandvik Coromant | |
| Tool | - | C4-TR-D13HCL-27050 |
| Insert | - | TR-DC1306S01515FWX 7115 |
| vc, m/min (ft/min) | 100 (328) | 160 (524) |
| fn, mm/rev (in/rev) | 0.20 (0.008) | 0.30 (0.012) |
| ap, mm (inch) | 0.15 (0.006) | 0.15 (0.006) |
| Tool life, pcs | 216 pcs | 300 pcs |
Customer case
Profiling with CoroTurn® TR, QS™ shanks
| Workpiece material | Stainless steel, M1.0.Z.AQ (200 HB) |
| Cutting tool, insert | QS-TR-D13JCR 2020HP, D1308 2025 |
| vc m/min (ft/min) | 200 (3.94) |
| fn mm/r (in/rev) | 0.18 (0.007) |
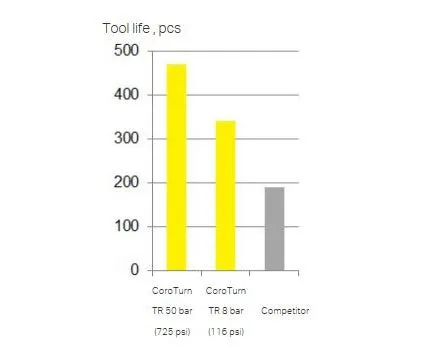
When changing to the CoroTurn® TR QS shanks, a customer could machine a remarkable number of components. As a result of implementing internal over- and under coolant, significant improvements were experienced both at high and low coolant pressures.
| Coolant, bar (psi) | 50 (725) | 8 (116) | External |
| Tool life, pcs | 470 | 340 | 190 |
Customer case
Precision hard part turning with CoroTurn® TR
Tool life
| Operation | External precision hard part turning |
| Component | Tripod (Spider) |
| Material | 16 MnCrS5 (58 – 62 HRc) |
| Tool | TR-SL-D13UCR-25 |
| Insert | TR-DC1308S01020F 7015 |
Challenge: The customer needed to develop an efficient solution for the external precision hard part turning. The aim was to achieve the surface finish and process capability within acceptable cost parameters.
Result:
- Lower cost per component and better process capability
- Consistent quality maintaining close tolerances as compared to other tools
- Improved tool life, from 70 to 200 pieces per edge
- Increased productivity by 31%
| vc m/min (ft/min) | 140 (459) | 150 (492) |
| fn mm/rev (inch/rev) | 0.07 (0.002) | 0.05 (0.0019) |
| ap mm (inch) | 0.3 (0.011) | 0.3 (0.011) |
| Result | ||
| Surface finish (Ra) | 0.5 | 0.5 |
| Tool life (pcs) | 200 | 70 |
| Time in cut (min) | 61.16 | 27.97 |
| Metal removal (Q) | 2.94 | 2.25 |
Create account chevron_right
Place orders, view prices and check tool availability
Subscribe to our newsletter chevron_right
Join us. Stay updated.

Sandvik Benelux B.V. - Division Coromant
+31108080280AB Sandvik Coromant, 811 81 Sandviken, Sweden